Capabilities

CNC milling,
engineered.

Four CNC mills — 3-axis, 4th-axis, and 5-axis — backed by in-house engineering, finishing, and inspection. Prototypes, bridge runs, and production, with one team accountable for your part.
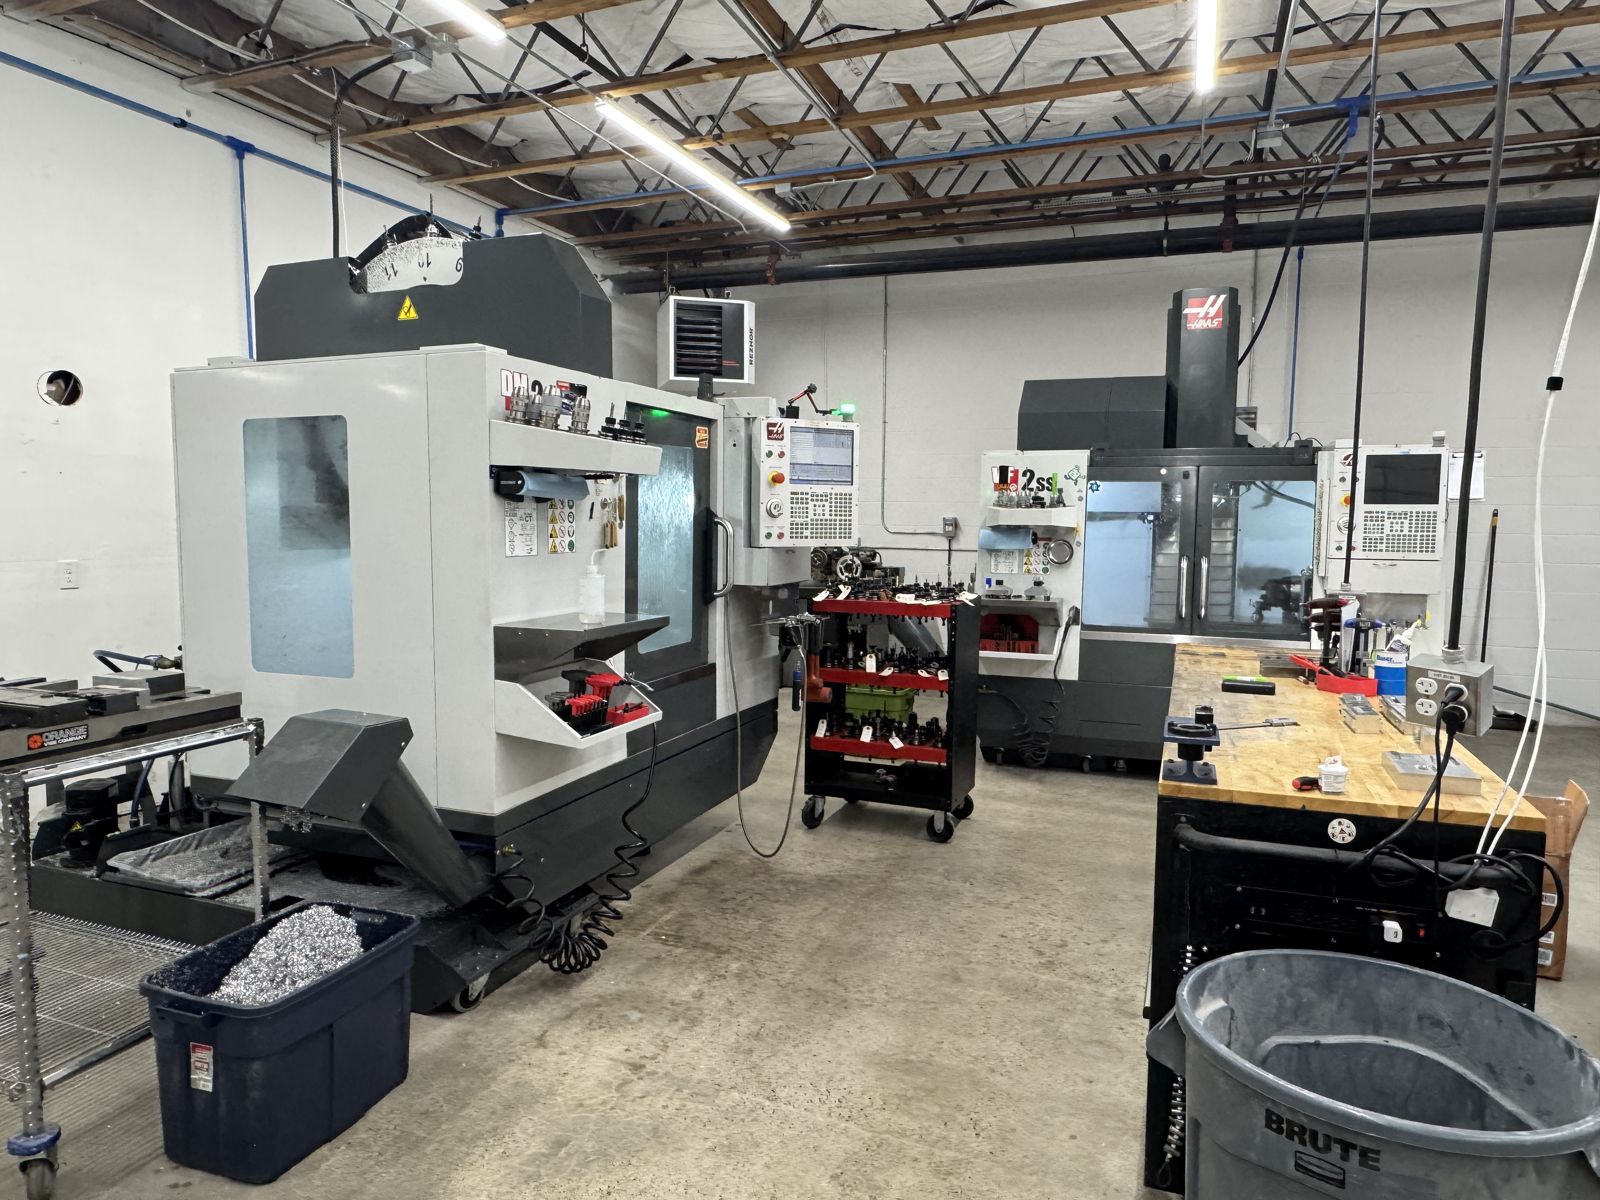
Row of Haas CNC mills on the shop floor

01 — CNC Milling

The right axis count for the part.

Plates, brackets, housings, fixtures, and complex multi-sided parts. We pick the machine and setup that hits the print with the fewest operations.
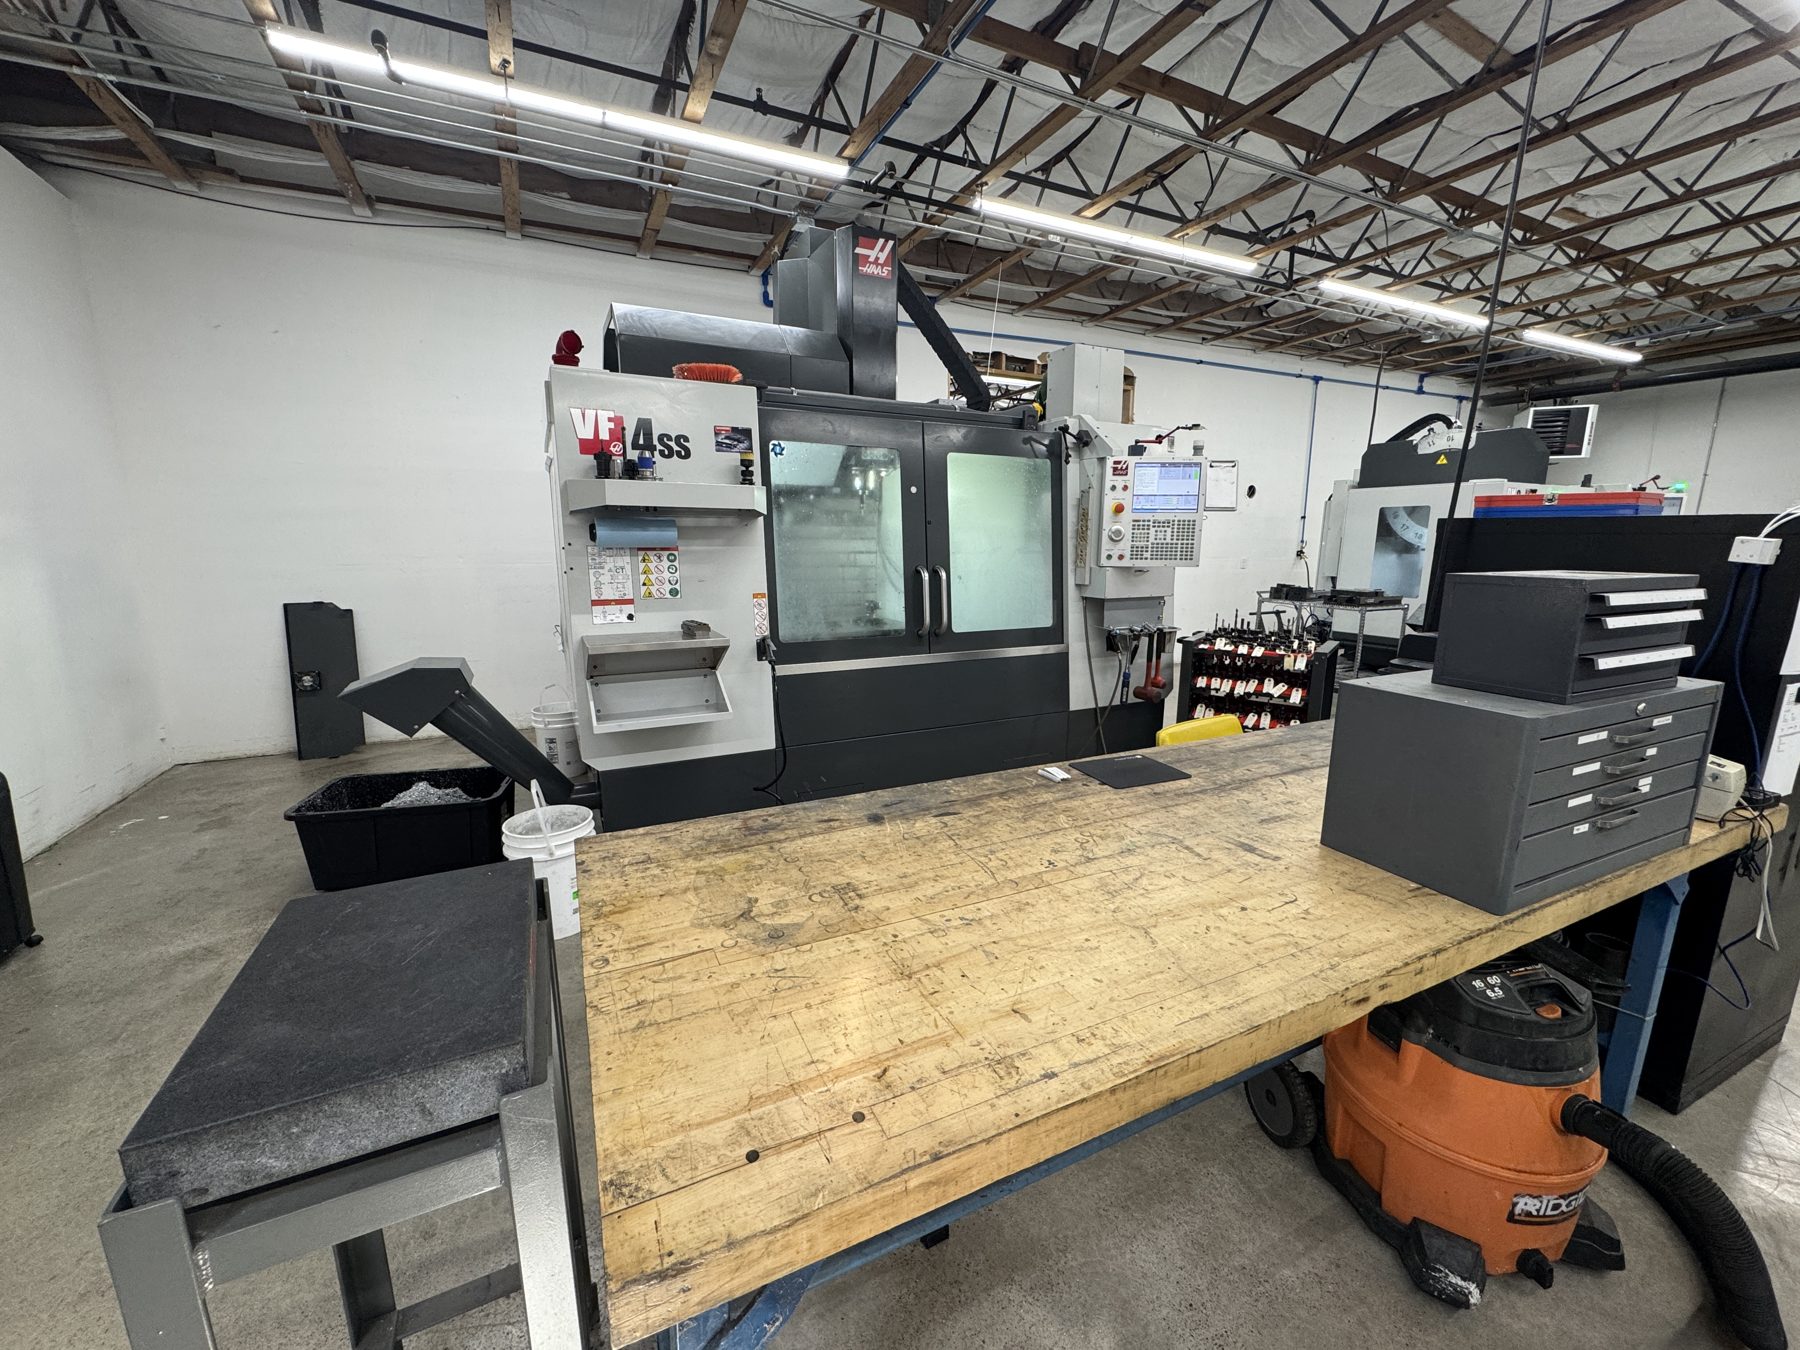
  • 3-axis ×2Haas VF-4SS and DM-2 for prismatic work, plates, and production runs.
  • 4th-axisHaas VF-2SS with a rotary for multi-side work and indexed features in one setup.
  • 5-axisLitz-Hitech LU-620 for complex geometry and fewer setups.
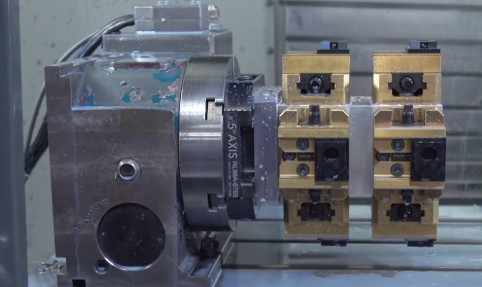
  • SetupZero-point workholding and dual-station vises for fast, repeatable changeovers. Spindle probing on the VF-4SS.
Haas mills installed on the Belfanti Machine Works shop floor
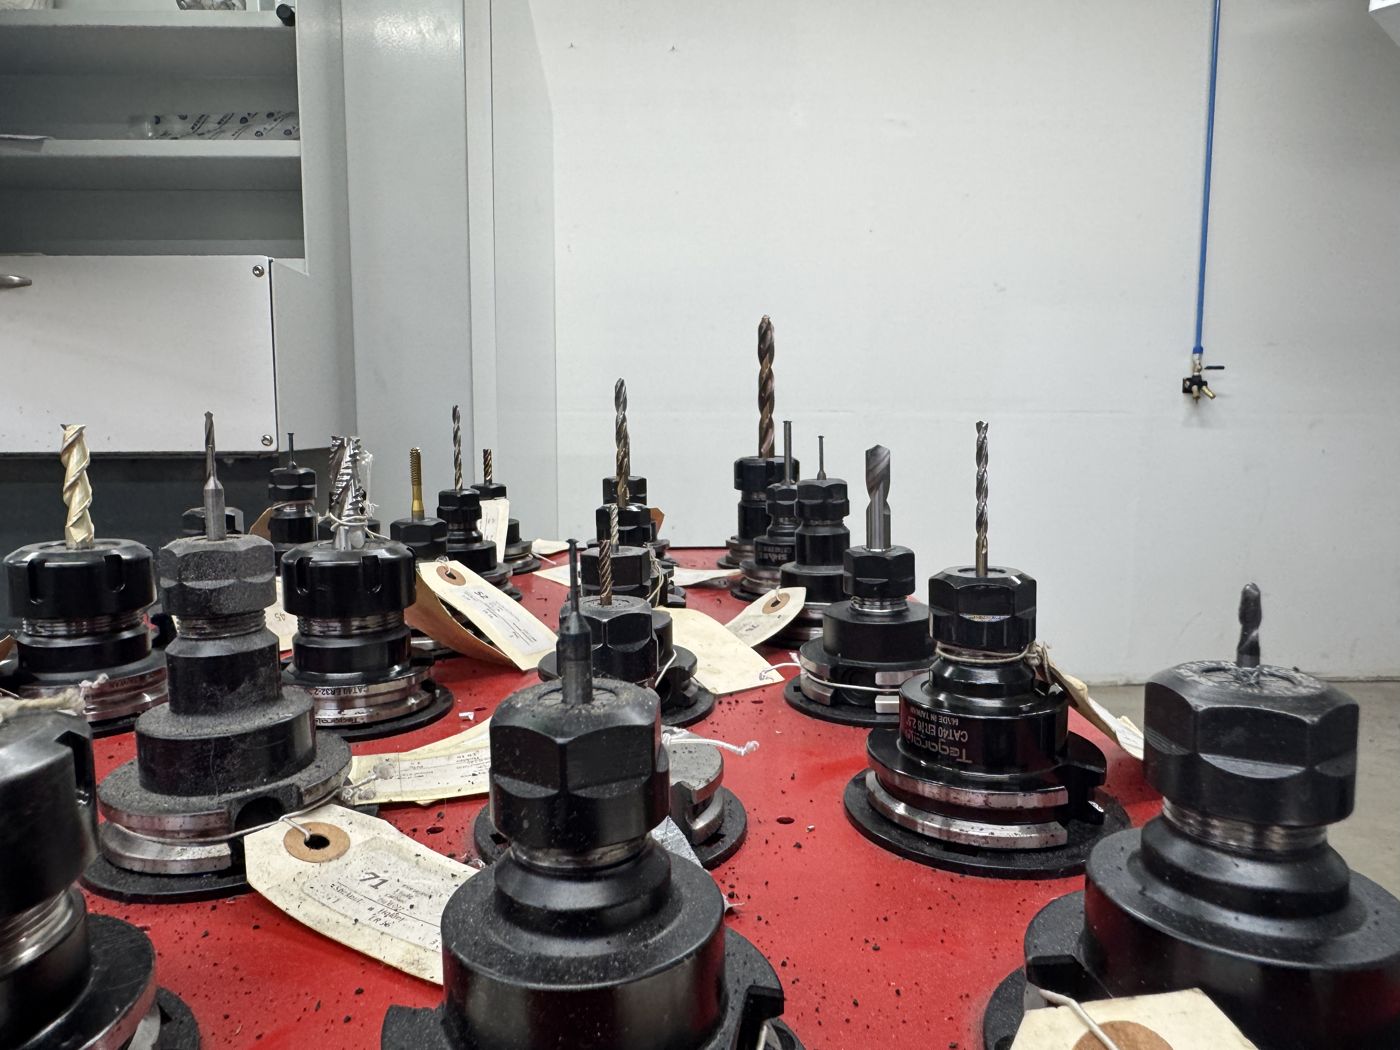
Tool holders staged on a cart
Tooling staged for the next job
4th-axis rotary with zero-point vises loaded
4th-axis rotary with zero-point vises
Pete at the workstation — CAD model on screen, marked-up print on the desk

02 — Engineering & DFM

We read the print like a design engineer.

25+ years of product engineering at Nike, Logitech, and Benchmade means we look past the dimensions to what the part has to do — and flag what's driving cost before we cut chips.

DFM on every quote

Tolerance, feature, and material notes that save money.

Fusion 360 CAD/CAM

Native CAD/CAM in-house. STEP, IGES, and PDF accepted.

Sketch to part

Bring a sketch or a rough model. We'll help make it machinable.

Fixtures & 3D printing

Markforged Onyx Pro for fixtures, soft jaws, and prototypes.

03 — Materials

Matched to what the part has to do.

If a cheaper material does the job, we'll tell you. Material certs available on request.

Material · Typical grades
General[Carbon steel, brass, Delrin, UHMW]
Aluminum[6061, 7075]
Stainless[303, 304, 316]
Composites[G10/FR4, carbon fiber] — plus carbon fiber layup molds
Select exoticsOn request — ask us
Finished aluminum parts, off the machine

04 — Finishing

Ready to install, not ready to rework.

Edge-break, surface, and marking in-house. Plating and heat treat coordinated through vetted partners, so you get one PO and one delivery.

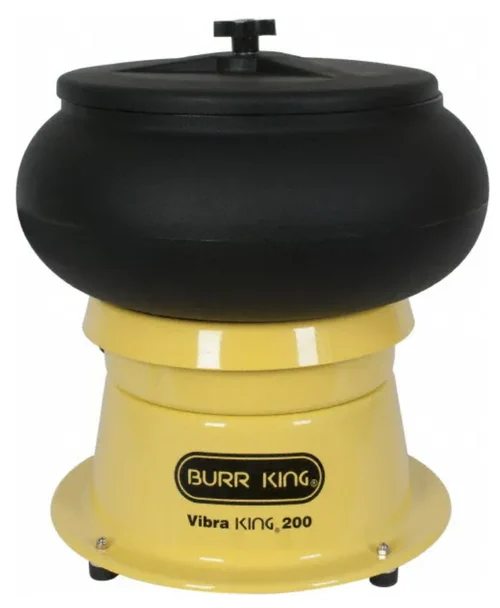
Vibratory finishing tumbler
In-house

Deburr & tumble

Hand deburr and vibratory tumbling for consistent edge-break.

Tray of bead-blasted aluminum parts
In-house

[Bead blast]

[Uniform matte finish, before or instead of anodize.]
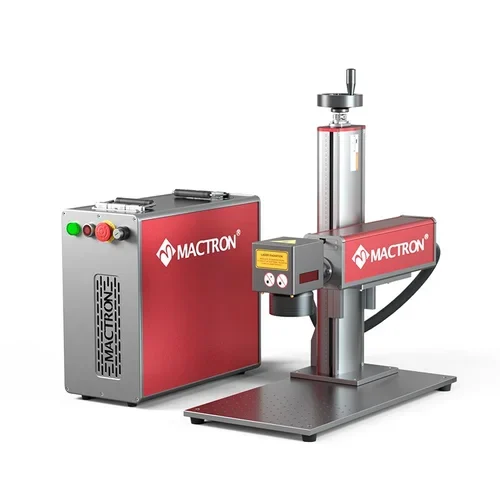
Fiber laser marking machine
In-house

Marking & engraving

50W fiber laser marking plus machined engraving for part numbers, logos, and serials.

Black-anodized parts, overhead
Partners

Anodize, plate, heat treat

Coordinated through vetted local vendors. One PO, one delivery.

05 — Inspection & QC
Checked before it ships.

±0.005"Standard
±0.001"Precision — or tighter
64 RaStandard finish, µin
  • First-article inspection on every new part
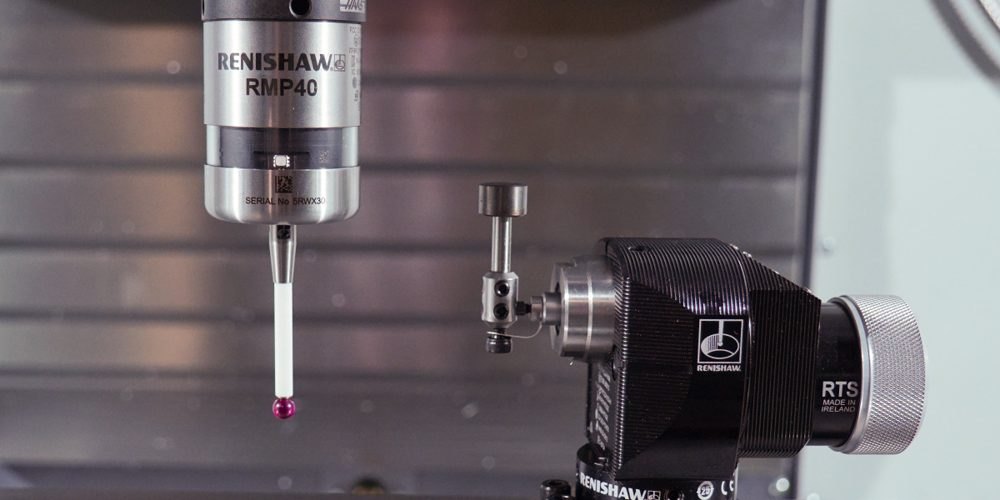
  • In-process spindle probing on the VF-4SS
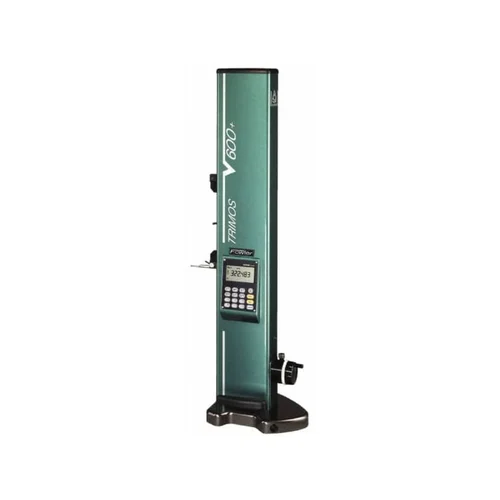
  • Trimos V600+ height gauge on a granite surface plate
  • [Inspection reports and material certs on request]
Trimos V600+ height gauge
Trimos V600+
Renishaw spindle probe and tool setter
Renishaw WIPS probing

Got a drawing?
Get a quote.

Send a STEP, IGES, or PDF. An engineer reviews it and comes back with price, lead time, and any DFM notes in 1–2 business days.